
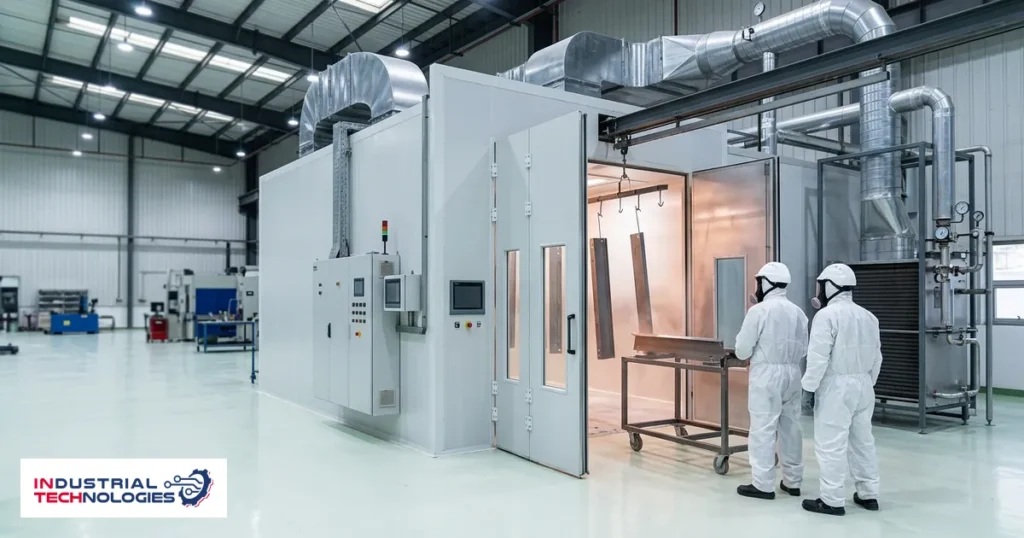
Asking what temperature the oven runs at is an incomplete question. An oven does not run at one temperature; it runs a curve: ramp up, hold, cool down. The curve decides surface quality, not the highest number in it.
The industrial coating heat curve is set by the coating in use rather than by workshop habit, and the delivered heat output in this family runs from 200,000 to 600,000 kcal/h.
Why the curve follows the material, not the part
Every finishing material behaves differently under heat: some need a long hold at a moderate temperature, others a fast ramp. The part decides how much heat is needed to bring it up to temperature; the material decides how far and for how long. Changing the coating in an existing plant can therefore require the curve to be reset even when the part has not changed.
Five heating systems and what tips the choice
| System | What tips the choice towards it |
|---|---|
| Diesel | Fuel availability and operation independent of the electrical supply |
| Gas | An existing gas supply on site |
| Electric heating | Available supply capacity and no on-site fuel handling |
| Heat pump | Electrically driven operation with no on-site combustion |
| Short-wave infrared | Heating the surface directly rather than the whole chamber |
Where the industrial part sits in this
Delivered configurations in this sector begin at a 3000×3000×3000 mm cabin for powder coating curing and reach 5700×3700×3000 mm for industrial baking ovens and above. The difference between the two is not size alone but what the heat is doing inside each.
Frequently asked questions
Does the curve change if the coating changes?
Yes, and that is the stated reason for setting the curve by the coating rather than by the part. A different material changes both the temperature required and the hold time, which is why the material is one of the four design inputs.
What needs to be sent to choose a heating system?
The finishing material in use, and the energy sources available on site: electrical supply capacity, and whether a gas supply exists. Those two narrow the choice among the five systems delivered.
Is a higher heat output better?
No. Heat output is derived from chamber volume and finishing material together, within a delivered range of 200,000 to 600,000 kcal/h. Output above what the chamber needs is running cost with nothing in return.
Are booths delivered with a controlled environment?
Temperature and humidity control together is delivered on custom booths whose coating requires a controlled environment, and the range is set per project by the finishing material and the part’s requirements.
Related reading
- Booth cycle time and line takt
- Continuous shift booth operation
- Four inputs for industrial booth design
Next step
Send the dimensions and weight of the largest part or platform to be coated, together with your site area, and the internal size and configuration come back against them. Talk to a specialist. The published range sits on the paint booths family page, and the sector configuration on the Industrial & Manufacturing sector page.